
Company profile
Automatically translated with DeepL.
Pulsar Photonics GmbH 是一家致力于激光技术领域的创新型高科技公司。该公司的服务范围涵盖激光加工技术、包含软件开发在内的设备制造,以及激光系统技术部门。
自成立以来,该公司一直致力于生产规模化方案的研究。 公司为客户提供从专业应用开发、量产准备到自动化生产设备制造,并包含售后服务及技术知识转移在内的全方位专属服务。Pulsar Photonics 持续投资于自身生产能力建设,致力于利用(超)短脉冲激光器进行单件和批量生产。核心工艺包括结构化加工、钻孔和精密切割。
Pulsar Photonics GmbH总部位于亚琛。该公司成立于2013年,是亚琛弗劳恩霍夫ILT研究所的衍生企业,其成长阶段的资金由波恩的高科技创业基金(HTGF)提供。 自 2021 年起,Pulsar Photonics 成为 Schunk 集团的一员。
这家员工人数略少于 100 人的公司发展迅速且盈利良好,是一家德国中小企业,同时也是“亚琛激光地区”(LaserRegionAachen)结构转型计划的成员之一。
Product areas 10
Industries
What's new 2
Laser-drilled filters and screens for industrial filtration processes
What are the challenges of filtering and screening with micro-perforations?
In many industrial filtration processes, such as material processing for the recycling industry, filters and screens play a central role: They remove particles and contaminants from the material stream, thereby safeguarding the quality of the end product and the stability of downstream processes.
However, high throughput rates, varying material qualities, and abrasive particles place high demands on filtration systems.
Typical challenges in the manufacture and application of industrial filters:
- Uneven filtration due to imprecise or varying pore sizes
- High pressure losses in the process, especially at high flow rates
- Rapid wear of filter structures caused by abrasive particles
- Uneven flow distribution within the filter
- Short filter service life
- Fluctuating quality of the final material
- Laborious filter changes/maintenance and plant downtime
- High material losses due to insufficient separation of contaminants
- Limited precision of conventional manufacturing processes for very small holes in the micrometer range
- Limited design freedom regarding hole diameters and hole geometries
- Clogging of filter openings by fine particles
Traditional manufacturing processes for filter structures quickly reach their limits, especially when dealing with high throughput rates, fine particle sizes, and heavily contaminated material streams.
Our Solution: Filter holes created by laser machining
Laser processing enables the production of high-precision holes in metals for filter and screen applications, such as those used in the recycling industry. Even very small hole diameters and high hole densities can be achieved with consistent results—a key requirement for stable filtration processes.
Compared to mechanical manufacturing processes, laser processing offers significant advantages for the production of modern filter structures:
- Contactless & burr-free machining with no tool wear
- Precisely defined hole diameters down to 100 µm and tight tolerances
- Reproducible filter geometries
- High hole densities for efficient filtration
- Flexible adaptation of hole patterns and filter designs
- Machining of all metals
- Uniform flow distribution thanks to precise, burr-free micro-drilling
- Longer filter service life and more stable process conditions
This allows filter systems to be tailored specifically to the requirements of demanding filtration processes - for example, in material reconditioning, polymer processing, or powder processing.
Machine Solution for precise laser drilling of filtration systems
Pulsar Photonics has developed a specialized line of laser systems for the industrial processing of filter plates and screens.
The RDX2Drill laser machine enables the precise automated laser drilling of large numbers of holes in filter structures.
Laser drilling redefined: Pulsar Photonics’ RDX2Drill works in single-pulse mode
Drilling thick metal sheets precisely and efficiently
Pulsar Photonics uses the single-pulse drilling process in the new RDX2Drill series to precisely and efficiently “shoot” holes in thick metal sheets. The plus: Sieves or filters made of high-strength materials and thick sheets can now also be micro-drilled with the laser. Such filters can therefore withstand high pressures or the strongest mechanical stresses.
Pulsar Photonics GmbH from Aachen deliberately uses single-pulse drilling for its RDX2Drill machine series. “These are high-energy pulses that do not work in an ultrashort pulse cycle, as is usually the case, but last microseconds or even milliseconds,” explains Philip Oster, Head of Laser Application Center. “They therefore have so much energy that each pulse basically shoots a hole in the material.”
If the laser “shoots” 50 holes per second …
Although the process does not have as many pulses per time as the ultrashort pulse laser, the speed is still impressive. For example, one user is currently running a process with 1.5 millimeter thick stainless steel sheet metal in which the RDX2Drill is laser drilling 50 holes per second. In his opinion, this value can be increased even further. The new system can therefore drill up to hundreds of thousands of holes with diameters of 100 to 400 micrometers in metallic materials with a material thickness of 0.5 to 1.5 mm with the utmost precision. Oster: “The efficiency and costs, primarily in the production of holes with diameters of around 200 micrometers, clearly speak for our laser drilling.”
A QCW (Quasi Continuous Wave) fiber laser with an output of several kilowatts perforates workpieces with a wavelength of 1060 to 1080 nm (infrared). One of the strengths is the combination of flexible system technology from the modular system with individual software. Oster: “One of our unique selling points is the Photonic Elements machine control system, which we have developed, designed and perfected exclusively for laser processing.”
Special software only for laser processing
Photonic Elements enables precise control and optimized process management, increasing the precision and efficiency of laser drilling. The digital control also allows you to switch quickly and easily between different component variants. This is a particular advantage for sieves and filters with high material thicknesses, which are subject to high pressure loads and require precise, customer-specific drilling patterns. Introducing this process was a challenge, emphasizes Oster: “With this melt-based process, we have to remove several hundred grams of melt per component. For this reason, the systems are equipped with an enclosure that surrounds the process area. The majority of the melt is extracted, collected and disposed of safely.
Automatic focus tracking instead of component distortion
The process generates a lot of heat in the component, which leads to distortion. Automatic focus tracking, which compensates for component deformations caused by thermal stress, for example, has proven itself as a countermeasure. With the purchase, the user is entering a complex technology that requires special training from the Aachen-based company: Nevertheless, it is worth getting started because the new RDX2Drill series is suitable for many applications: for example, sieves and filters for waste water filtration, hydrogen production, recycling and energy generation.
Videos 1
Images 4
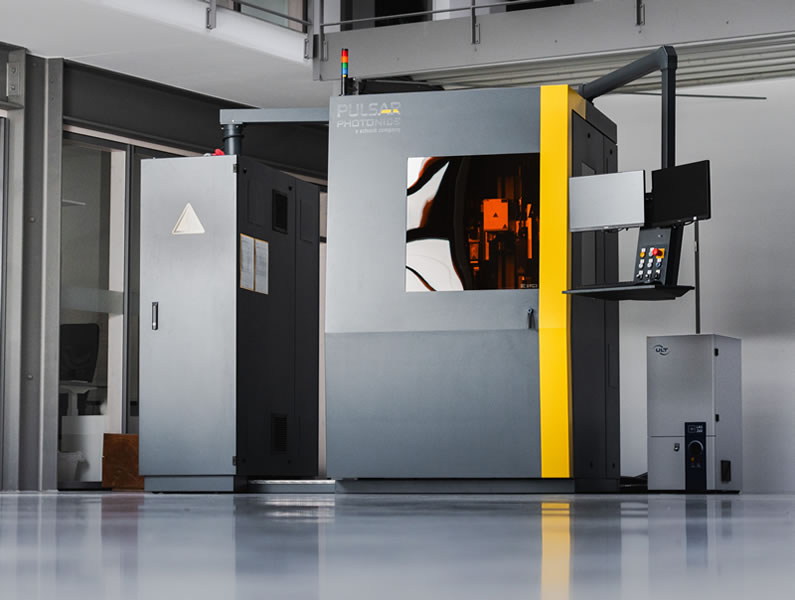
RDX2Fiber Laser Drilling Machine
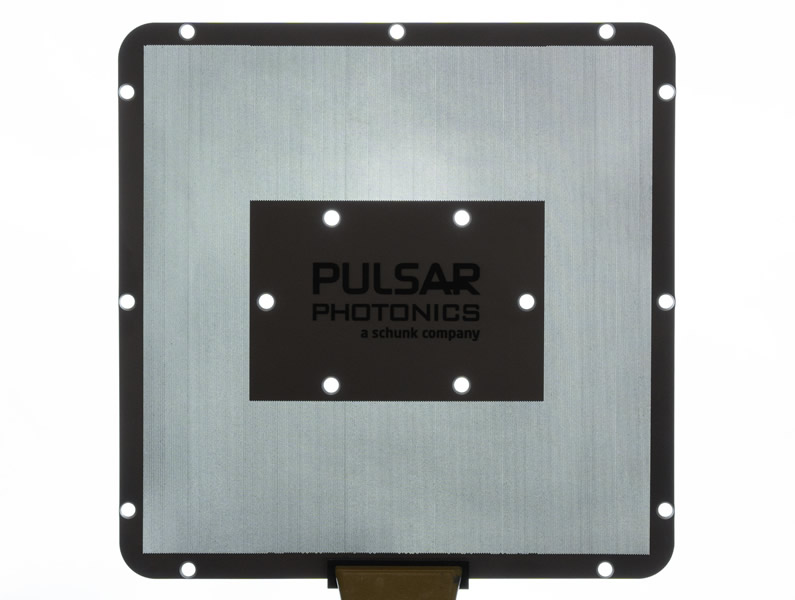
50 holes every second: The RDX2Drill series enables the drilling of 100 to 400 micrometer holes in metallic materials with high precision.
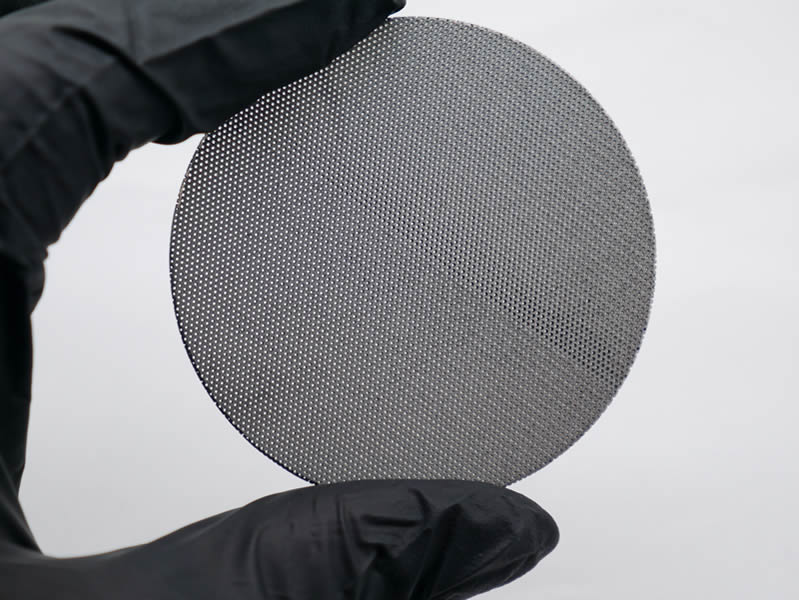
Filter application
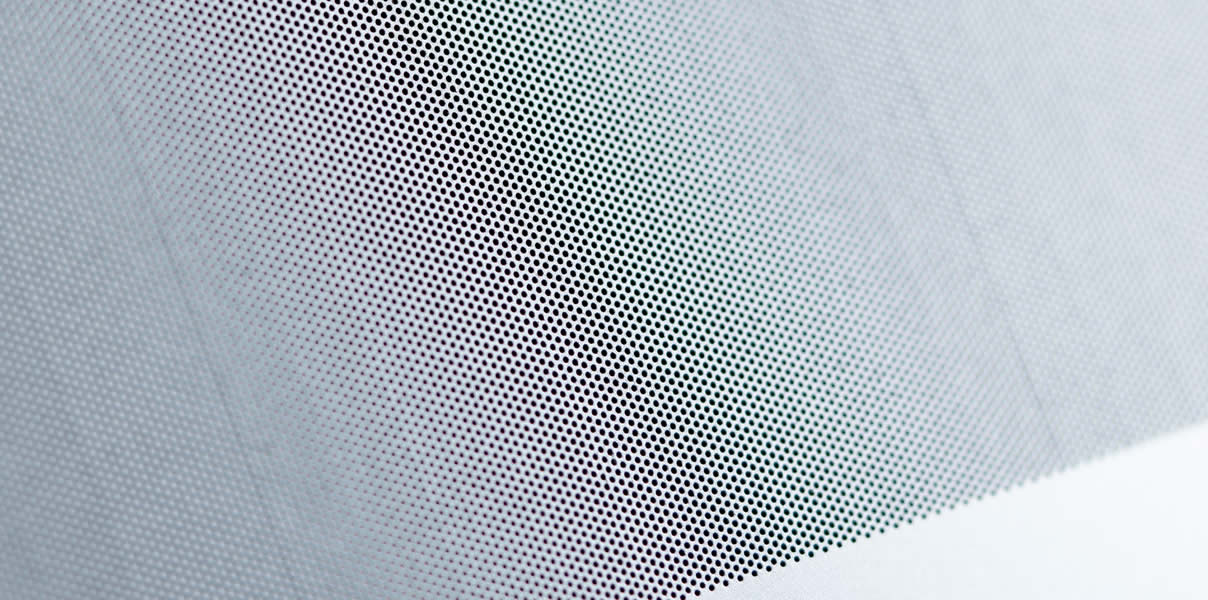
Laser drilling